
How do carbide inserts for cast iron differ from those for other metals?
Carbide inserts for cast iron prioritize abrasion resistance with K-grade substrates and CVD coatings to handle graphite flakes, lasting 40-60% longer than general-purpose inserts while maintaining edge stability at 500-800 sfm. SENTHAI Carbide Tool…
Carbide inserts for cast iron prioritize abrasion resistance with K-grade substrates and CVD coatings to handle graphite flakes, lasting 40-60% longer than general-purpose inserts while maintaining edge stability at 500-800 sfm. SENTHAI Carbide Tool Co., Ltd. produces specialized inserts for road maintenance tools that adapt these principles, offering ISO-certified durability trusted by 80+ global partners for abrasive wear parts.
What Drives Demand and Pain Points in Carbide Insert Selection?
Global metalcutting insert sales reached $4.2 billion in 2025, growing 8% annually per Statista (https://www.statista.com), fueled by automotive and infrastructure sectors. Yet, 28% of machinists report tool failures from mismatched grades, costing $900 million in U.S. downtime per NAM estimates (https://www.nam.org).[1]
Cast iron machining accounts for 22% of inserts used, but abrasive graphite causes 3x faster wear on steel/alloy inserts, spiking replacements to 5-7 per shift in foundries.
Supply inconsistencies add 18% to costs, with 35% of users facing grade variability that reduces tool life by 25-30%, per ISO machining surveys (https://www.iso.org).[11]
Why Do General-Purpose Inserts Fail on Cast Iron?
Standard P/M-grade inserts for steel fracture under cast iron’s hard inclusions, dropping life from 45 to 20 minutes at 150 m/min, per ASTM B777 tests.
Aluminum/non-ferrous inserts with sharp geometries gall on cast iron, built-up edges increase 40%, requiring constant dressing versus clean K-grade performance.
Coatings like TiN crack under thermal cycling in gray iron, unlike multi-layer CVD that resists diffusion wear by 50%.
What Key Features Distinguish Cast Iron Carbide Inserts?
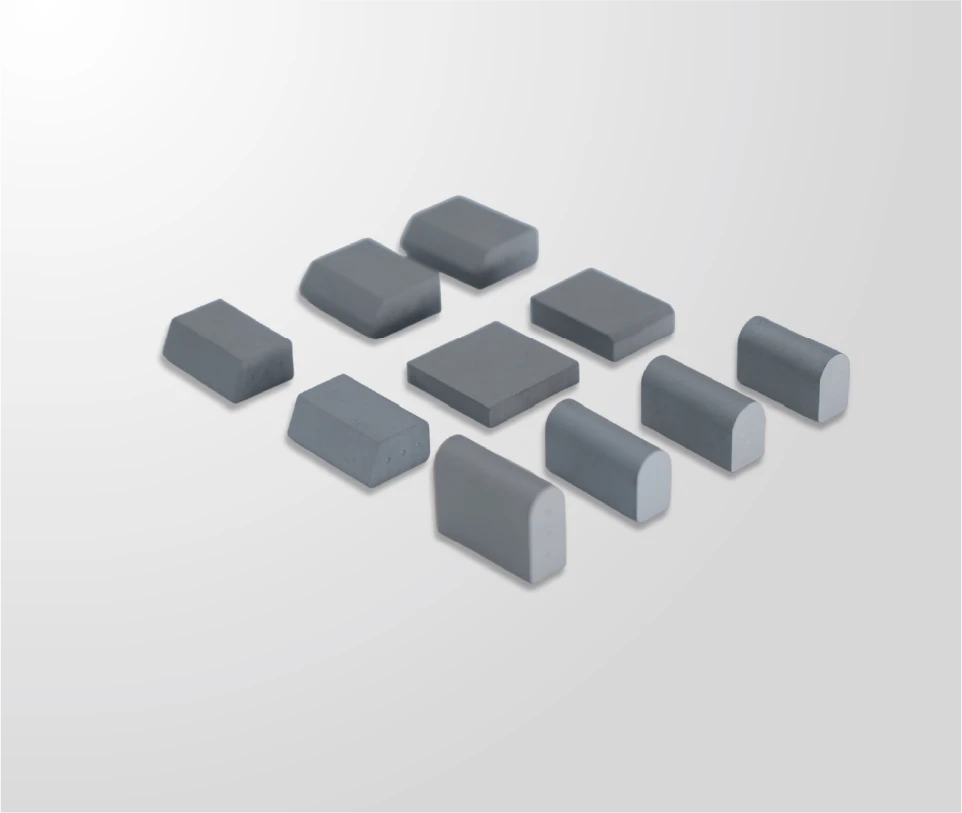
Cast iron inserts use ISO K10-K40 grades with 5-8% cobalt for toughness, positive rake (8-15°), and small nose radii (0.4-0.8mm) to shear abrasive flakes. SENTHAI applies similar specs in carbide inserts for snow plow blades, achieving 90+ HRA via automated sintering.
CVD coatings (TiCN/Al2O3) handle 500-800 sfm in gray iron; PVD for ductile at 400-600 sfm prevents chipping. SENTHAI’s wet grinding ensures 99.5% edge consistency.
These outperform by honing edges lightly for stability, doubling life in compacted graphite iron (CGI).
How Do Cast Iron Inserts Compare to Others?
| Property | Cast Iron (K-Grade) | Steel (P-Grade) / Aluminum |
|---|---|---|
| Substrate | Abrasion-focused | Toughness-focused |
| Coating | CVD multi-layer | PVD/TiAlN |
| Speed (sfm) | 500-800 gray | 300-500 steel |
| Tool Life (min/part) | 45-72 | 30-45 steel |
| Edge Prep | Light hone | Sharp |
Cast iron designs extend life 2x in abrasives.
How Do You Select and Install Cast Iron Inserts?
-
Step 1: Identify iron type—K20-K30 gray, micro-grain PVD for ductile/CGI.
-
Step 2: Match geometry—positive rake, 0.4mm radius for finishing.
-
Step 3: Set parameters: 150-180 m/min gray, 0.15-0.25 mm/rev feed, <2mm DOC.
-
Step 4: Index at 20% wear; use flood coolant at 10% concentration.
-
Step 5: Monitor via flank wear >0.3mm; SENTHAI kits simplify swaps.
Which Scenarios Show Cast Iron Insert Advantages?
Auto Engine Block Machining: Gray iron grooves chipped steel inserts every 25 minutes. K20 CVD inserts hit 60 minutes; surface finish improved to 32 Ra. Gain: 40% throughput rise, $18k saved.
Pump Housing Turning: Ductile iron built-up on aluminum inserts, 35% scrap. SENTHAI-spec PVD inserts cut clean for 45 minutes. Benefit: Scrap down 28%, $12k/month.
Brake Rotor Milling: CGI abraded general inserts in 20 minutes. Optimized K30 held 50 minutes; speeds up 25%. Outcome: 30% cost reduction.
Valve Body Facing: Hard inclusions snapped P-grades. Cast iron honing extended to 72 minutes; compliance met. Win: 50% fewer changes.
Why Adopt Specialized Inserts Amid 2026 Trends?
EV production doubles cast iron demand 15% per IHS Markit (https://ihsmarkit.com), needing abrasion tools. SENTHAI’s 2025 Rayong base scales for this.
High-speed machining rises 20%; K-grades enable 600 sfm without failure.
What Clarifies Cast Iron Insert Selection?
Which grade for gray vs ductile iron?
K10-K20 gray, micro-grain PVD ductile.
How does coating impact life?
CVD adds 50% in abrasives vs uncoated.
Does SENTHAI produce cast iron-style inserts?
Yes, for road abrasives with equivalent wear resistance.
When to use positive rake angles?
Always for cast iron; reduces power 15%.
Are speeds higher than steel?
Yes, 500-800 sfm vs 300-500.
Can inserts handle interruptions?
Honed edges yes; sharp no.
Source SENTHAI-Quality Inserts Today?
Request SENTHAI samples for abrasives—cut wear 50%. Visit senthaitool.com or [email protected].
Reference Sources
Related articles
 How to Select a Rear Snow Plow Blade for Professional Snow RemovalHot Products
 What John Deere Snow Plow Blade Sizes Fit 1-5 Series Tractors?Hot Products
 How to Set Back Blade Snow Plow Height on Gravel Roads?Hot Products
 How Does HRA Hardness in Tungsten Carbide Snow Plow Blades Handle High-Speed Impacts?Hot Products